Why Do You Need a Paint Spray Booth?
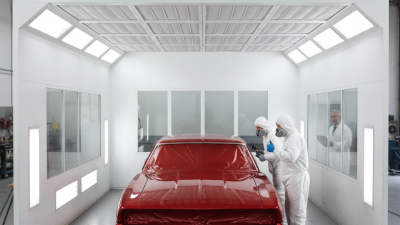
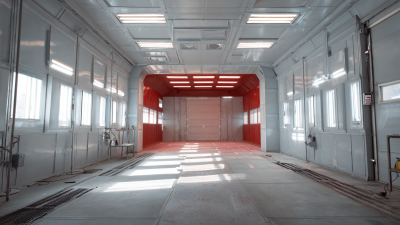
A paint spray booth does more than hold paint and equipment. It creates a controlled space where airflow, lighting, and filtration help produce a cleaner, more consistent finish. Picture a freshly primed panel under bright booth lights. The air moves steadily past it, carrying overspray toward filters instead of letting it settle back onto the wet coating. That difference can mean fewer dust nibs, less rework, and a more predictable result.
The booth also helps separate finishing work from sanding dust, shop traffic, and changing room conditions. Its fans, filters, and maintenance schedule all matter. A booth is not a magic box. Clogged filters or poor airflow can undermine the finish and create avoidable exposure concerns. Even a small shop should treat inspection and housekeeping as part of the process. Details count.
A verified quotation from a named paint-booth expert was not supplied, so I won’t invent one. For publication, add a sourced statement from a qualified coatings or ventilation specialist. That matters because booth design depends on the work, coating system, and facility. The right setup may improve finish quality and workflow, but it also requires informed selection and regular upkeep. Is every shop using its booth as effectively as it could? Often, the answer deserves a closer look.
What a Paint Spray Booth Is and How It Works
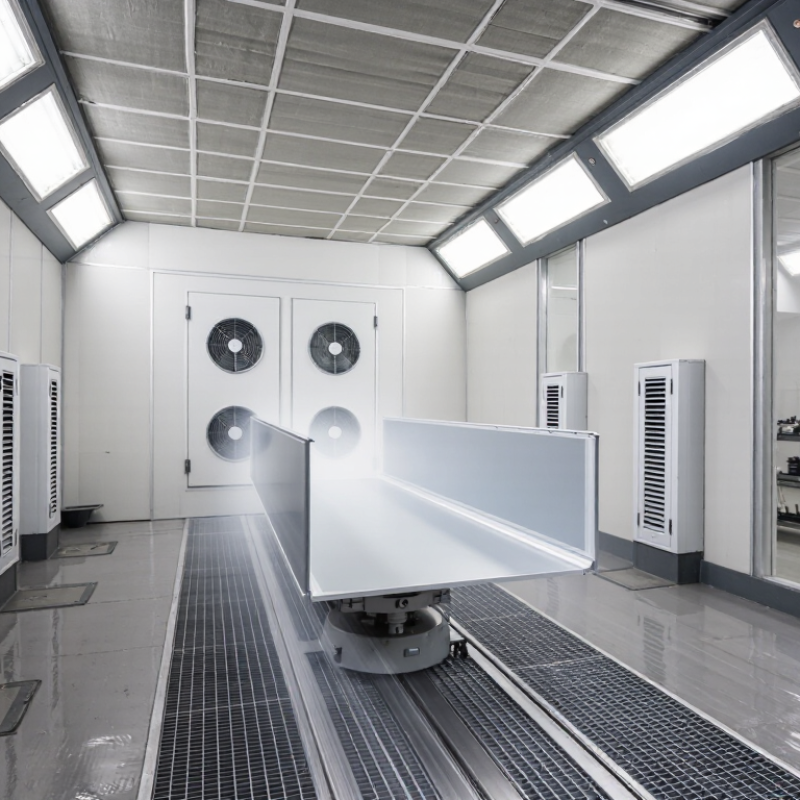
A paint spray booth is an enclosed, ventilated workspace designed for controlled coating application. It separates spraying from nearby people, tools, and surfaces. The enclosure usually includes walls, lighting, exhaust fans, intake filters, and exhaust filters. Its purpose is not simply to make painting look tidy. It manages airborne overspray, vapors, and dust while giving the coating a more predictable path to the workpiece. The exact setup depends on the coating, object size, and local safety requirements.
During spraying, clean air enters through an intake system. Air moves across the work area and carries particles toward the exhaust side. Filters capture overspray before air leaves the booth. Suitable ventilation also helps reduce vapor buildup. A balanced airflow pattern matters. Too little airflow can leave haze and uneven finishes. Too much airflow may dry the coating too quickly or waste material. Technicians should check filters, fan performance, and pressure readings before each shift. Small checks prevent larger defects.
The booth also improves finishing consistency. With steady lighting and controlled airflow, an operator can notice runs, dry spray, and missed edges earlier. It can reduce contamination on wet surfaces and limit exposure to airborne substances when operated correctly. Still, a booth is not a substitute for training, protective equipment, or maintenance. In practice, airflow is rarely perfect. Door gaps, clogged filters, and careless loading can change results. That detail deserves honest attention. Qualified professionals should verify the design, electrical equipment, fire protection, and operating procedures against applicable safety codes.
How a Booth Controls Overspray and Airborne Contaminants
Why Do You Need a Paint Spray Booth?
A paint spray booth controls overspray by directing contaminated air away from workers and nearby surfaces. Without controlled airflow, fine droplets can settle on floors, lights, tools, and freshly coated parts. The U.S. Environmental Protection Agency’s AP-42, Surface Coating Operations, reports conventional air-spray transfer efficiency at roughly 20–30%. The remaining material may become airborne overspray. That waste is visible. Smaller particles are easier to miss.
A properly designed booth uses intake air, exhaust fans, filters, and balanced airflow. OSHA’s 29 CFR 1910.94(c) requires mechanical ventilation for spray-finishing operations and addresses airflow, exhaust, and fire prevention. A booth should pull contaminants through the filter path, not push them toward an operator’s breathing zone. Clean filters matter. Loaded filters increase resistance and can weaken capture performance. In daily use, airflow may change faster than expected.
Practical checks reveal problems early. Watch for paint dust on nearby ledges, uneven coating, unusual fan noise, or a rising pressure reading. These signs deserve investigation. A booth cannot correct poor spray technique, excessive coating pressure, or neglected maintenance. EPA data also shows that higher-transfer application methods can reduce material loss, but equipment settings still matter. Real workshops are imperfect. Doors open, filters clog, and operators adjust habits under pressure. Good booth performance depends on measuring airflow, replacing filters on schedule, and reviewing conditions regularly.
How Ventilation and Filtration Protect Workers
A paint spray booth controls where contaminated air goes. Its ventilation pulls overspray, solvent vapors, and fine particles away from the worker’s breathing zone. OSHA’s Technical Manual identifies adequate airflow as a core control for spray-finishing hazards. In many open-face booth designs, OSHA requires an average face velocity of at least 100 feet per minute under 29 CFR 1910.94(a). Air movement must be steady, not merely powerful.
That difference matters. Filters capture airborne paint particles before they reach exhaust equipment or nearby surfaces. They also reduce deposits on lights, walls, and workers’ clothing. However, standard particulate filters do not remove every vapor. Their performance depends on filter type, airflow, loading, and maintenance. NIOSH’s industrial hygiene guidance supports combining engineering controls with exposure monitoring, rather than trusting one safeguard.
A booth is not magic.
During a real shift, a clogged filter can make the fan sound strained while airflow weakens at the operator’s face. A simple pressure reading can reveal this change earlier. OSHA recommends maintaining ventilation systems and inspecting spray areas regularly. NFPA 33 also emphasizes controlling ignition sources and managing combustible residues in spray operations. These details are easy to overlook.
Workers still need suitable respirators, protective clothing, and training based on the coating and exposure assessment. Ventilation protects best when the spray pattern stays inside the capture zone. Overspray outside that zone signals a process problem, not just a dirty filter. Better booth design helps, but disciplined daily checks matter more than impressive equipment.
How a Controlled Environment Improves Paint Finish Quality
Why Do You Need a Paint Spray Booth?
How a Controlled Environment Improves Paint Finish Quality
Paint rarely fails because of color alone. The surrounding air often decides whether a finish looks refined or uneven. A paint spray booth creates a controlled space for this work. Stable airflow carries overspray away from the surface. Filtered air also limits dust settling into wet paint. That difference becomes visible under bright inspection lights. Small particles can resemble tiny craters, especially on dark coatings. The booth cannot fix poor preparation. It gives preparation a fair chance.
Temperature and humidity matter just as much. When the air is too cold, paint may level slowly and retain texture. Excess moisture can affect drying and surface appearance. A monitored booth helps technicians keep conditions within the coating maker's specified range. This supports repeatable results across different days and projects. It also improves visibility. Even lighting reveals dry spray, runs, thin edges, and missed areas before the part leaves the work zone. Experienced operators still check panels from several angles. One view can be misleading.
Safety and reliability are connected to finish quality. Proper extraction reduces airborne contaminants and supports a cleaner working atmosphere. Regular filter changes, airflow checks, and temperature records make the process easier to verify. These details sound ordinary. They are not. A booth is not a magic box. A rushed cleaning step or incorrect spray distance can still ruin a smooth coating. Real workshops face changing weather, equipment wear, and human judgment. Controlled conditions reduce those variables, but they never remove the need for skill.
Why Do You Need a Paint Spray Booth?
How a controlled environment improves paint finish quality and supports safer spraying
A spray booth provides controlled airflow that helps capture overspray, reduce airborne dust, and create more consistent coating conditions. The chart shows OSHA 8-hour permissible exposure limits for common solvents used in coating applications; lower limits require tighter ventilation and exposure control.
Reference: U.S. OSHA Table Z-1 permissible exposure limits. Values are 8-hour time-weighted averages in parts per million (ppm).
Which Projects and Workplaces Benefit from a Spray Booth
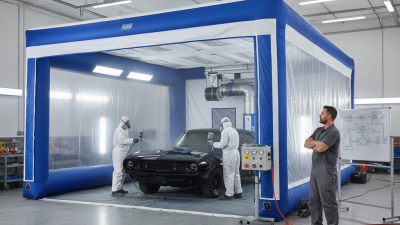
A paint spray booth is useful wherever coatings, overspray, and airborne vapors meet daily work. Auto repair shops use booths for bumpers, doors, and full vehicle refinishing. Furniture makers need them for cabinets, tables, and detailed wood finishing. Metal fabricators also benefit when applying primers, protective coatings, or industrial finishes.
OSHA’s 29 CFR 1910.107 recommends at least 100 linear feet per minute of airflow through spray booth openings. That figure gives managers a measurable ventilation target. The number is practical, not decorative. A booth can keep dust away from wet paint and guide contaminated air toward filtration. In my experience, even a small enclosure improves consistency when the floor is clean and the lighting is direct.
Industrial maintenance rooms, production workshops, and educational laboratories may also need spray booths. NFPA 33 addresses fire protection and ventilation for spray application areas. Its guidance supports careful separation from ignition sources, storage areas, and ordinary workspaces. A booth is not magic. Filters still clog, fans still fail, and operators sometimes rush inspections. That weakness deserves attention. Workplaces using solvent-based or catalyzed coatings should assess exposure controls, respiratory protection, and local requirements before installation. Small custom shops often overlook replacement-filter costs. That mistake can undermine both air quality and finish quality.